Explore our CE-approved industrial-grade waterproof equipment, high-output power systems, and outdoor protective hardware engineered for global distributors and brand owners.
In modern outdoor equipment manufacturing, maritime electronics transport, and tactical gear procurement, achieving hermetic waterproof reliability requires strict adherence to polymer material science, radio-frequency (RF) welding physics, and European Union CE standard compliance. As leading OEM/ODM manufacturers and exporters since 2011, our engineering facility produces technical dry bags, waterproof backpacks, and protective enclosures built to withstand continuous hydrostatic submersion and extreme environmental stress.
Key Takeaway for B2B Procurement Teams: Standard stitched and taped seams deteriorate over time when exposed to UV radiation and salt hydrolysis. Industrial-grade CE Certified dry bags utilize high-frequency electromagnetic molecular bonding (RF Welding) to create seamless, monolithic barrier structures rated up to IPX8 (submersion under pressure beyond 3 meters).
Selecting the optimal composite material directly influences flex fatigue life, cold-crack temperature tolerance, and abrasion durability. Our R&D team manufactures products using two core elastomeric materials engineered for demanding B2B applications:
| Technical Property | TPU Laminated Ripstop Nylon | 500D/1000D PVC Tarpaulin | Testing Standard |
|---|---|---|---|
| Hydrostatic Head Pressure | > 25,000 mm H₂O | > 20,000 mm H₂O | ISO 811 / AATCC 127 |
| Tensile Strength (Warp/Weft) | 2800 N / 2400 N | 2500 N / 2200 N | ISO 13934-1 |
| Low-Temperature Crack Point | -40°C (-40°F) | -25°C (-13°F) | ASTM D2136 |
| UV Degradation Resistance | Grade 4.5 (500 hrs) | Grade 4.0 (500 hrs) | ISO 4892-2 Xenon Arc |
| Environmental Compliance | REACH, RoHS, PFAS-Free | RoHS, Low-Phthalate | EU Regulation 1907/2006 |
Mechanical stitching inherently pierces fabric, introducing thousands of micro-perforations that degrade barrier integrity. To guarantee absolute waterproof performance under CE EN 60529 standards, our manufacturing lines utilize automated 27.12 MHz High-Frequency Radio Energy Welding.
Under precise pressure and high-frequency electromagnetic oscillation, polymer molecules at the joint interface melt and intermingle at a molecular level. Upon cooling, the seam retains 100% of the parent material's tensile strength, eliminating glue failure, tape peeling, and micro-channel air leakage under pressure.
Utilizes stiffened polypropylene top bars. When folded downward three times and latched via UTX Duraflex® side-release buckles, it forms a mechanical compression gasket that repels heavy sea sprays, rainstorms, and rapid surface submersion.
Incorporates vulcanized teeth and airtight polyurethane teeth-interlocking seals. Tested to withstand up to 0.5 bar pressure (5 meters underwater submersion) for extended protection of sensitive electronics, cameras, and laptops.
Understanding key market shifts enables wholesale buyers, brand directors, and importers to make strategic inventory and product specification choices.
Global regulatory pressure (such as the EU Eco-Design Regulation) is accelerating the demand for eco-conscious materials. Supply chains are migrating toward 100% recycled PET (rPET) base fabrics laminated with solvent-free, bio-derived TPU membranes without compromising tensile or burst strength.
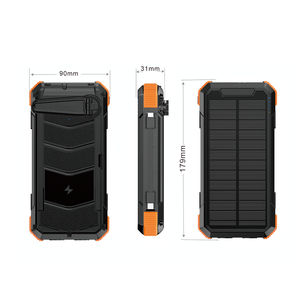
Modern consumers demand active functionality. Future-ready dry bags incorporate flexible solar charging panels (integrated with 20000mAh power banks), internal Qi wireless charging pockets, magnetic mounting brackets, and built-in IPX7 Bluetooth audio drivers.
The boundary between technical outdoor survival gear and daily urban commuting is dissolving. High-growth lines feature sleek matte finishes, padded breathable EVA back panels, ergonomic laptop sleeves, and modular MOLLE attachments combined with IPX7 waterproof protection.
Founded in 2011, our manufacturing enterprise has evolved from specialized consumer electronics audio and power accessories into a multi-category engineering power-house. Managing hundreds of SKUs across personal audio, high-speed GaN chargers, protective laptop backpacks, and hermetic outdoor dry bags, we offer brand owners a single, highly vetted manufacturing partner for their product catalog.
Since our inception in 2011 with flagship sound systems and heavy-duty audio gear, our in-house engineering and design teams have refined manufacturing processes to maintain consistent tolerance standards across large-scale export production.
Every dry bag, sealed pack, and electronic accessory undergoes rigorous batch testing: 100% air-pressure inflation leak detection, hydrostatic water immersion chamber testing, and mechanical buckle load testing prior to packaging.
We supply full technical compliance documentation including CE Mark Declaration of Conformity, EN 60529 Ingress Protection Test Reports, REACH SVHC compliance certificates, and RoHS testing for smoothly clearing customs in North America, Europe, and Asia-Pacific.
From custom pantone color dyeing and high-frequency logo embossing to custom molded hardware, internal padded organizers, and retail-ready packaging design, our R&D facility provides end-to-end prototyping within 7 to 10 days.
To avoid costly product recalls, seam separation, or customs holds, international buyers must evaluate potential manufacturing facilities against four key quality dimensions:
Find instant answers regarding minimum order quantities, manufacturing lead times, CE compliance certificates, and custom OEM processes.
Upgrade your product catalog with CE Certified, high-frequency welded waterproof gear, fast-charging solutions, and outdoor tech accessories. Contact our engineering team today for instant quotations, factory audits, and OEM sample requests.