Explore our vetted collection of high-volume OEM/ODM export hardware, tactical packs, fast chargers, and smart peripherals designed for global technology distributors.
The global carry gear and bag manufacturing industry has undergone a radical transformation. Driven by modern urbanization, the surge in digital nomadism, international business travel, and heightening personal security concerns in major transport hubs, anti-theft backpacks have evolved from a niche specialty accessory into a core product category for mainstream retail and consumer tech brands.
Modern commercial procurement officers, OEM brand managers, and B2B buyers no longer evaluate anti-theft backpacks based solely on basic aesthetic design or simple zipper enclosures. Today's search intent and procurement guidelines demand high-level information gain across material science, anti-cut standard compliance (EN388 Level 4/5), electromagnetic RFID signal shielding, smart IoT integration, TSA-accepted lock mechanisms, and ISO-certified manufacturing ethics.
This industry whitepaper provides international procurement directors and wholesale buyers with a deep, data-driven analysis of the world's leading suppliers and exporters. By combining manufacturing expertise established since 2011 with rigorous supply chain auditing practices, this guide serves as an essential framework for identifying reliable manufacturing partners, optimizing landed unit costs, and capitalizing on upcoming market growth.
The following detailed profile highlights the world's top ten manufacturers and exporters leading the industry in production capacity, technical innovation, anti-theft patents, and OEM/ODM service standards.
Founded in 2011, Volkano has grown from pioneering personal audio devices and protective gear into a world-class OEM/ODM powerhouse across 9 core product categories. Renowned for its dedicated in-house R&D team, Volkano integrates advanced cut-proof textiles, concealed YKK zippers, and built-in smart charging ports into ergonomic business and travel backpacks.
Core Strengths: Comprehensive product ecosystem (bags, power banks, computing peripherals, TWS audio), flexible MOQs, low RMA rates, and complete export compliance for North America and EU markets.
Headquartered in the Netherlands with extensive manufacturing infrastructure in Eastern China, XD Design popularized the iconic Bobby Anti-Theft Backpack series. They specialize in multi-layer cut-resistant structures, hidden pocket geometries, and recycled PET fabrications.
Core Strengths: Strong consumer brand equity, award-winning industrial design, and commitment to sustainable eco-friendly raw materials.
Pacsafe is globally recognized for setting the technical security benchmark in luggage and travel bags. Utilizing patented eXomesh® stainless steel wire fabric overlays, ToughGear locking systems, and RFIDsafe™ blocking pockets, they target high-end travel retail networks.
Core Strengths: Unmatched physical intrusion resistance, military-grade anti-cut mesh integration, and global distribution network.
Korin Design focuses on tech-integrated minimalist urban packs like the ClickPack and FlexPack series. They excel in integrating retractable wire lock systems, magnetic quick-release shoulder straps, and waterproof rain-cover fabrics.
Core Strengths: Sleek futuristic aesthetics, compact volume efficiency, and strong popularity among corporate tech gifts.
Located in Fujian Province, China's bag production hub, this manufacturing enterprise operates over 40 production lines specializing in high-volume, cost-competitive luggage exporting for global department stores and big-box retailers.
Core Strengths: Aggressive unit pricing for bulk orders exceeding 50,000 units, extensive fabric sourcing networks, and fast sample turnaround.
Nomatic has established a strong market footprint by combining functional anti-theft storage with versatile expansion systems. Key features include TSA-ready 180-degree flat opening, magnetic water bottle pockets, and internal perimeter locks.
Core Strengths: Maximum organization capability, heavy-duty tarpaulin material construction, and strong brand presence in North America.
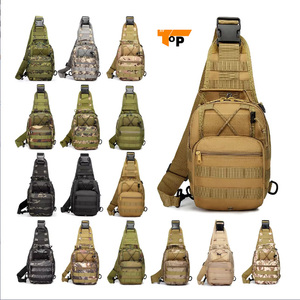
Specializing in heavy-duty ballistic 1680D nylon, tactical sling bags, and outdoor security packs, Everest Leather offers contract manufacturing for military, outdoor adventure, and industrial supply brands.
Core Strengths: Extreme durability standards, waterproof heat-welded seams, and custom tactical webbing integration.
Focusing on sustainable smart travel gear, TravelCraft combines recycled ocean plastics (RPET) with solar panel charging flaps, anti-theft combination zippers, and hidden back-panel passport vaults.
Core Strengths: Eco-conscious brand marketing, integrated renewable energy accessories, and ergonomic airflow back panels.
While known for legacy hardshell suitcases, Samsonite's contract OEM division exports premium anti-theft laptop backpacks featuring RFID-blocking executive slots, Kevlar-reinforced corners, and integrated TSA combination cables.
Core Strengths: Uncompromising quality control standards, worldwide repair network support, and premium business market appeal.
Operating out of Ho Chi Minh City, VinaBag provides global exporters with competitive tariff-free shipping options to major Western markets under various free trade agreements. They produce cut-proof commuter packs and student anti-theft bags.
Core Strengths: Strategic geographic advantage for duty exemption, strong sewing craftsmanship, and reliable international freight links.
The modern anti-theft backpack relies on a combination of advanced textile engineering, structural security, and integrated electrical components. B2B buyers must understand the primary security features currently defining the market:
Engineered using ultra-high-molecular-weight polyethylene (UHMWPE), Kevlar strands, or woven stainless steel mesh layered beneath 600D/1680D Polyester. Meets EN388 Level 4 and Level 5 blade cut standards.
Zipper tracks inverted and hidden against the user's back panel eliminate unauthorized access in crowded spaces. Utilizing YKK double-layer anti-puncture zipper teeth prevents ballpoint pen penetration.
Metallic foil woven linings inside dedicated card and passport pockets block 13.56 MHz frequencies, protecting credit cards and biometric passports from unauthorized RFID/NFC skimming devices.
When placing OEM/ODM orders, specifying the correct fabric blend and hardware components is critical to balancing security standards with landed pricing targets:
| Feature Category | Standard Specification | Premium Security Upgrade | Commercial Benefit |
|---|---|---|---|
| Outer Fabric | 600D Water-Repellent Polyester | UHMWPE Cut-Proof Fabric (Level 5) | Eliminates razor-slash theft in transit |
| Zipper Hardware | Standard Nylon Coil #5 | YKK Anti-Puncture Double Zipper + TSA Lock | Prevents sharp object intrusion & lock-picking |
| Internal Lining | 210D Polyester | 210D RPET + Faraday RFID Blocking Pockets | Protects digital data & enhances eco-credentials |
| Power Integration | USB 2.0 Passthrough Port | USB-C PD 65W Passthrough + Solar Charging | Enables fast laptop/phone charging on the go |
| Locking Mechanism | Zinc Alloy Zipper Pull Locks | Built-in TSA 007 Cable Lock System | Complies with global airport security regulations |
Over the next five years, the anti-theft backpack industry will experience structural shifts driven by technological integration and regulatory sustainability mandates:
With Western markets introducing stricter environmental packaging and textile regulations (such as the EU Sustainable Textiles Strategy), major B2B buyers are shifting away from virgin polyester. Leading factories are adopting Global Recycled Standard (GRS) certified RPET derived from post-consumer water bottles, bio-based TPU coatings, and fluorine-free DWR (Durable Water Repellent) treatments.
Traditional combination locks are rapidly giving way to smart locking systems. Future-proof product lines incorporate low-energy Bluetooth (BLE) proximity alarms, Apple Find My / Android Find My Device tracking modules, and biometric fingerprint TSA latches capable of storing multiple user profiles with sub-second unlock times.
Distributors increasingly prefer consolidated suppliers capable of offering bundled tech gear. Rather than sourcing bags from one supplier and power electronics from another, procurement managers favor suppliers like Volkano who manufacture matched suites of carry bags, high-capacity GaN fast chargers, TWS wireless earbuds, and portable power banks designed to fit seamlessly into dedicated bag compartments.
Since launching in 2011 with the flagship Bazooka Bluetooth Speaker and Boom Series Aux Headphones, Volkano has expanded into an international manufacturer managing hundreds of active SKUs across audio, power, wearables, computer peripherals, and ergonomic bags. This deep cross-category experience gives global B2B buyers a distinct competitive advantage:
By producing both technical carry bags and power accessories under one roof, Volkano guarantees 100% hardware compatibility. Power bank pockets are precision-stitched to fit high-density external batteries, while built-in cable passages support maximum charging efficiency without strain.
Our dedicated team of industrial designers and textile engineers continually introduces value-driven, trend-setting designs. From initial 3D rendering and fabric cut testing to final prototype approval, we accelerate your time-to-market by up to 40%.
Every anti-theft backpack batch undergoes rigorous testing: zipper cycle tests (10,000+ pulls), drop testing, strap tensile loading (up to 25kg), and cut-resistance validation. All products are fully supported by published warranty terms, giving distributors complete peace of mind.
We cater to both entry-level volume retail lines and flagship premium series (such as our elevated VolkanoX range). We support full OEM customization, including custom silicone badge branding, custom zipper pulls, customized box packaging, and tailored Pantone fabric dyeing.
For standard catalog models with custom logo branding, our typical MOQ starts at 500 units per colorway. For fully customized fabric specifications, bespoke mold development, or custom Pantone dyeing, the baseline MOQ is generally 1,000 to 2,000 units depending on material availability.
Our cut-proof fabrics are tested in accordance with international EN388 standards using automated blade tension testing machinery. We provide third-party laboratory test reports (SGS, TUV, or ITS) certifying cut resistance levels ranging from Level 3 to Level 5 based on client specifications.
Yes. However, international air and ocean freight transport regulations require power banks containing lithium-ion batteries to comply with UN38.3, MSDS, and dangerous goods transport standards. Alternatively, we offer "Power-Ready" backpacks fitted with internal USB/USB-C wiring harnesses, allowing end-users or distributors to insert power banks post-import.
All factory production operates under AQL 2.5 Major / 4.0 Minor inspection guidelines. Our inline QC teams inspect raw material tear strength, seam stitching density, zipper smoothness, TSA lock functionality, and barcode label accuracy before final carton sealing.
Once tech packs and 2D/3D design files are confirmed, physical sample production typically takes 7 to 10 business days for standard fabrics, and 14 to 20 days if specialized custom molds or unique hardware treatments are required.
Our production facilities maintain ISO 9001 quality management system certification, BSCI social compliance auditing, and compliance with EU REACH and US California Proposition 65 chemical safety regulations.
To ensure maximum margin performance and minimize aftermarket returns, procurement teams should review this evaluation checklist before finalizing supplier contracts:
| Audit Dimension | Critical Test Benchmark | Risk Mitigation Target |
|---|---|---|
| Structural Integrity | Strap tensile pull test > 250N for 1 minute | Prevents strap failure under heavy laptop loads |
| Security Hardware | TSA lock combination reset cycle > 3,000 attempts | Eliminates lock jam defects at retail point-of-sale |
| Weather Resistance | Hydrostatic head water resistance > 5,000mm | Protects internal laptop and tablet electronics |
| Color Fastness | ISO 105-B02 Light fastness Grade 4 or higher | Prevents fabric fading under intense solar exposure |
| Packaging Resilience | ISTA 1A Drop test standard (10 drop cycles) | Ensures master cartons survive international ocean freight |
Whether you are planning a high-volume retail product launch, expanding your consumer electronics carry ecosystem, or seeking dedicated private-label OEM/ODM production, our team of experts is ready to assist you.
Contact Us